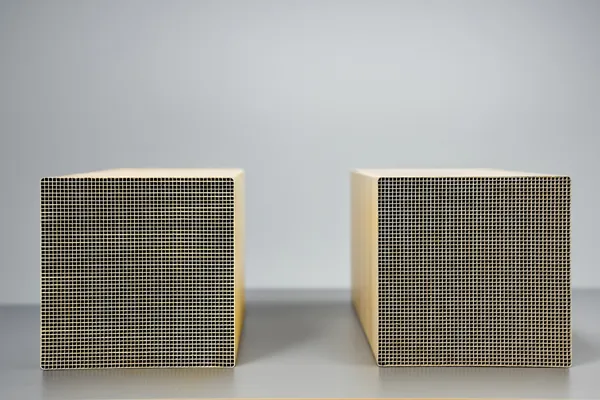
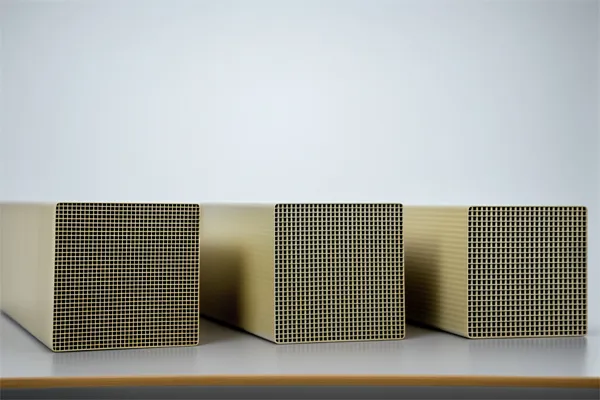
Strong ultra-low temperature activity: applicable temperature 150–350°C (efficiency ≥85% at 150–160°C, ≥90% at ≥160°C)
Excellent resistance to alkali (alkaline earth) metal poisoning, excellent sulfur resistance, and strong hydrophobicity
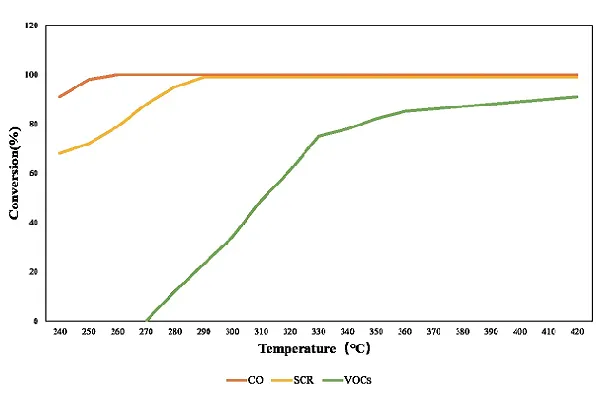
Full temperature range from 240°C to 380°C
High activity at low temperature: CO removal efficiency ≥80% at 240°C
Energy saving and efficiency improvement, reducing operating costs
Strong resistance to poisoning and strong hydrophobicity
Three-in-one: CO + NOx + VOCs
Simultaneous removal of CO, NOx, and VOCs at 280–420°C
Fewer catalyst layers, reducing retrofit costs
Direct replacement for existing SCR systems
Combines low-temperature adaptability, tolerance to complex operating conditions, and synergistic multi-pollutant control
High activity at low temperature; reaches optimal operating range starting at 240°C
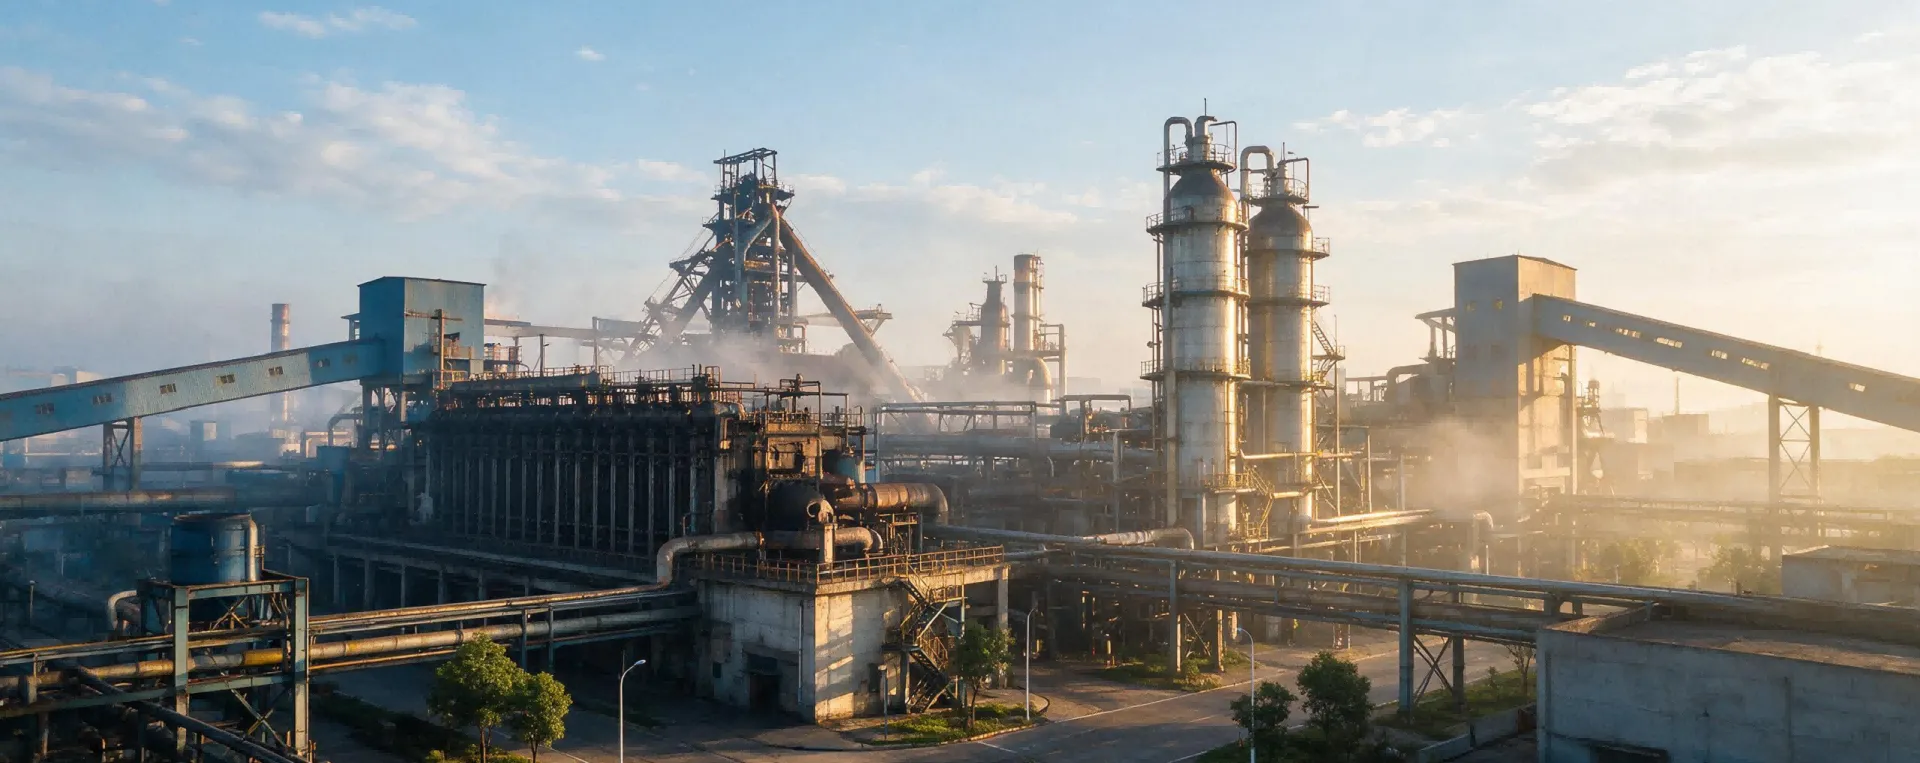
Applicable to 240–420°C operating conditions, covering typical temperature fluctuations in coke oven flue gas
Adaptable to environments with coexisting components such as SO₂, NOx, high humidity, aromatics, and alkanes
Retains partial SCR functionality to synergistically reduce NOx and ammonia slip
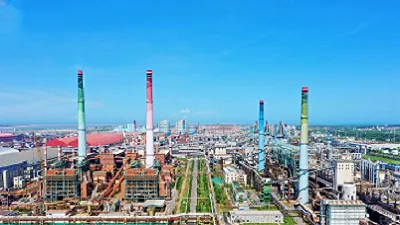
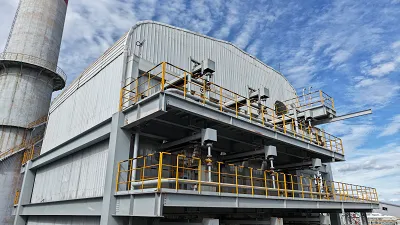
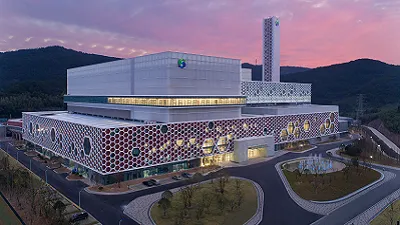
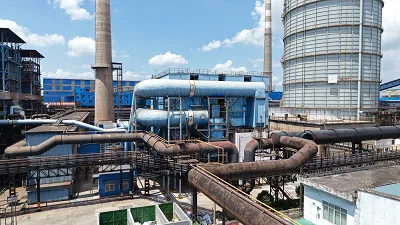
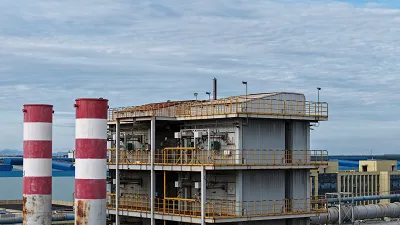
Projects covering more than 20 industries, with over 800 cases worldwide.
Providing customized solutions for different flue gas conditions
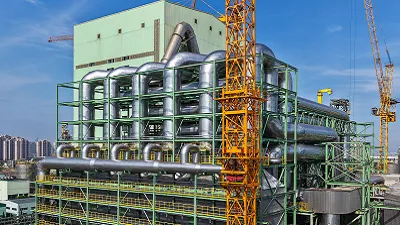
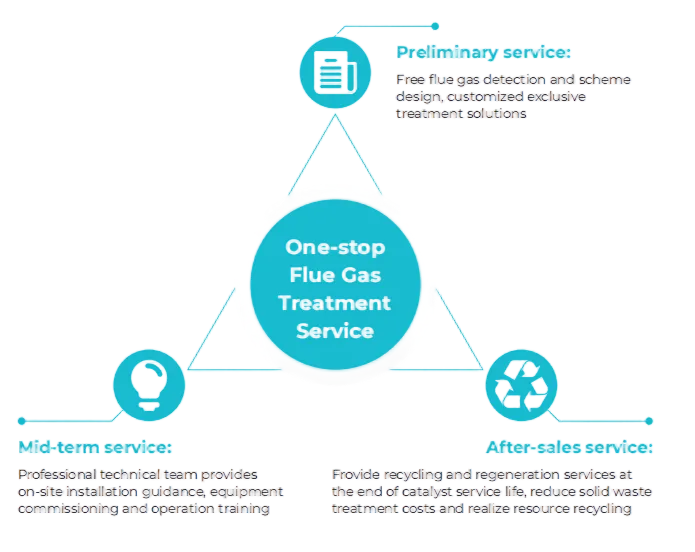
Providing customers with one-stop, full-process flue gas treatment services
TONEXUS Environmental Protection Technology Co., Ltd., established in 2006 and listed on the Shenzhen Stock Exchange Main Board (Stock Code: 003027), upholds the corporate philosophy of “Toward Net-Zero, Beyond Industry.” The company is committed to becoming a globally recognized strategic partner in pollution reduction, carbon mitigation, and industrial net-zero transformation, contributing TONEXUS’s technological expertise to the world’s green transition. Its core business areas cover Flue Gas Treatment (EPC & Catalysts), CCUS, and the R&D and production of new energy materials and equipment, serving key sectors such as steel, power generation, coking, construction materials, chemical industry, non-ferrous metals, waste incineration, pulp and paper, and renewable energy.
International-leading low-temp SCR denitration (60% energy-saving), 6 patented techs, and advanced CO2 absorption solvents TX-1 solving amine oxidation.
20,000m³/year catalyst production across 3 specialized plants + 100,000㎡ eco-equipment facility enabling full-chain solutions.
Class-A design/engineering licenses, National Green Factory title, 200+ patents, and multiple national science awards.
800+ successful projects across 20+ industries, validated by global industrial decarbonization partnerships.